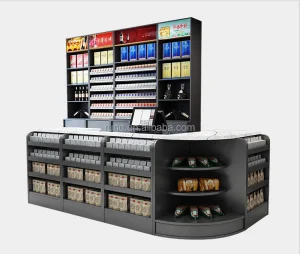
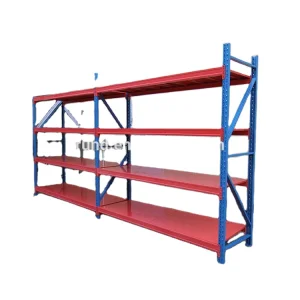
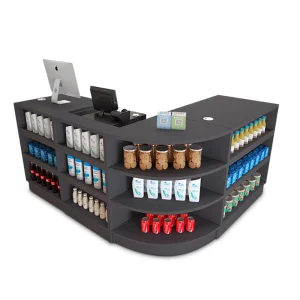
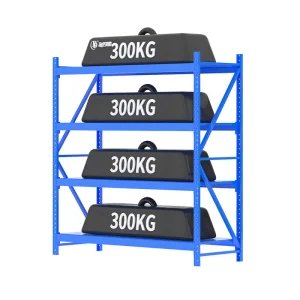
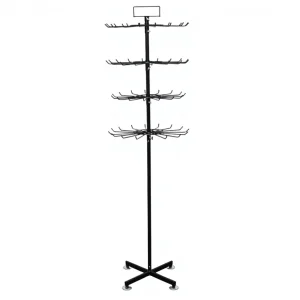
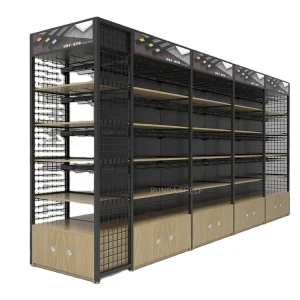
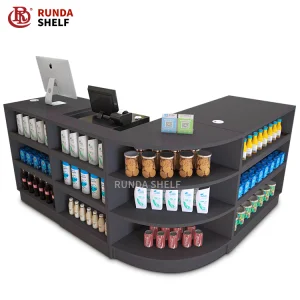
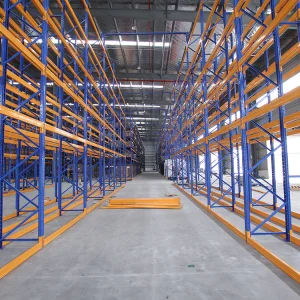
In the modern era of Industry 4.0, global supply chains demand more than just hardware; they require certified safety, structural integrity, and logistical efficiency. As a leading exporter, Shenzhen Runda ensures that every CE-certified product meets the rigorous safety standards required by international markets, minimizing liability and optimizing warehouse throughput.
We leverage a network of over 1,200 partners to maintain agile production, ensuring that even during global fluctuations, your procurement remains stable.
By integrating laser cutting and automated painting, we achieve unparalleled precision and durability in every shelf and rack unit.
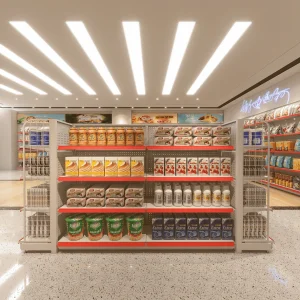
From hyper-market layouts to dense warehouse storage, our designs are optimized for local seismic and usage requirements.
Established in 2015, Shenzhen Runda Racking Manufacturing Co., Ltd. has evolved into a premier manufacturer specializing in heavy-duty industrial shelving. With over 11 years of industry expertise and 9 years of global export experience, we serve 3PL operators and enterprise buyers worldwide. Our 35,000 sqm facility and 18-member R&D team ensure that we lead the market with 120+ new product releases annually.
 Runda Racking