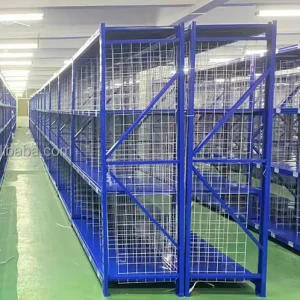
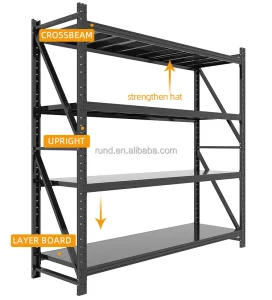
In the rapidly evolving landscape of global logistics, the role of a specialized Warehouse Storage Shelf Manufacturer extends far beyond simple steel fabrication. As global supply chains face unprecedented pressure for efficiency, China’s industrial storage manufacturing hubs, particularly in Shenzhen, have emerged as the nexus of innovation, cost-scalability, and agile OEM/ODM engineering. Leveraging a mature ecosystem of Q235 and Q355 steel supply chains, manufacturers like Shenzhen Runda provide a distinct "Information Gain" for procurement officers by integrating advanced seismic modeling and corrosion-resistant surface chemistry into standard pallet rack production.
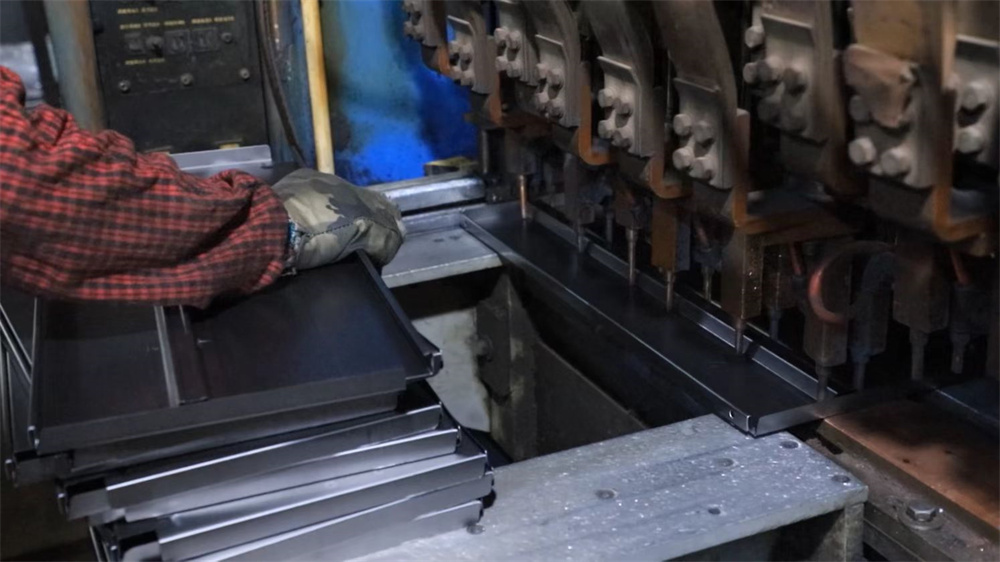
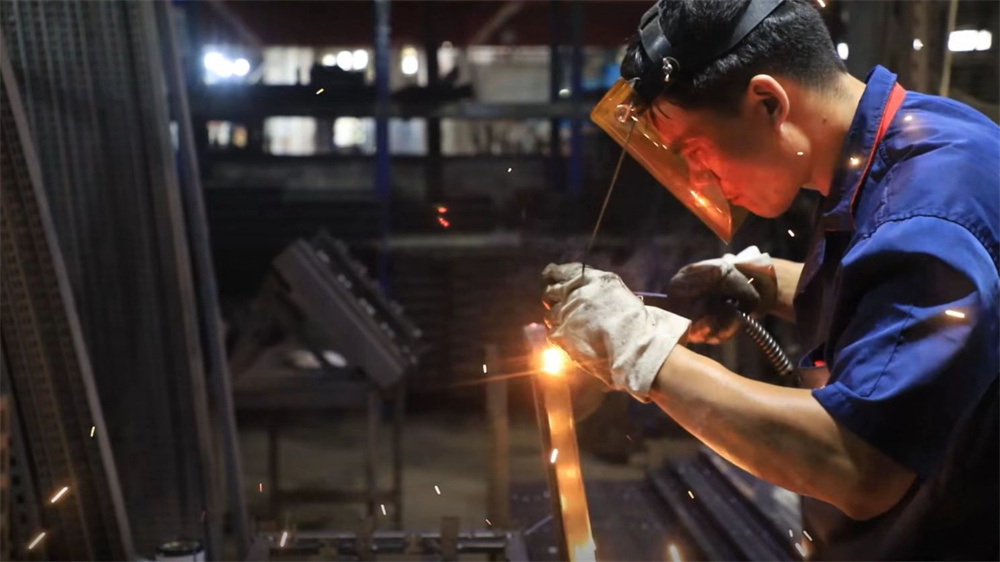
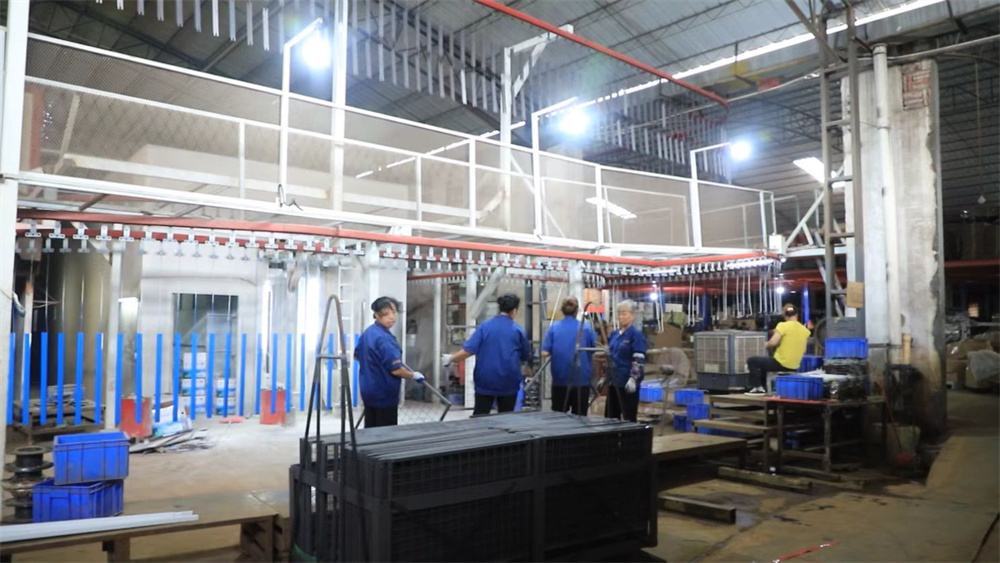
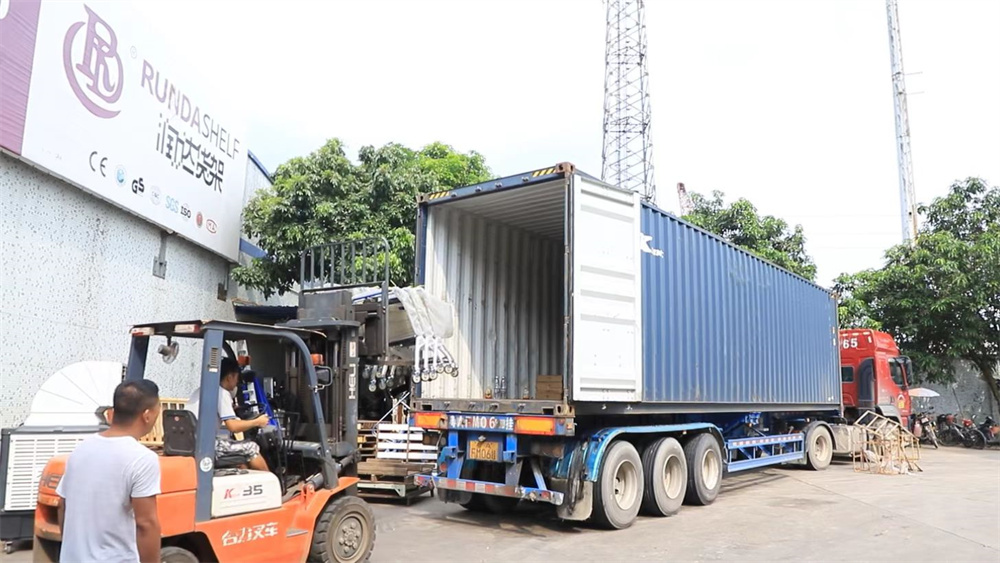
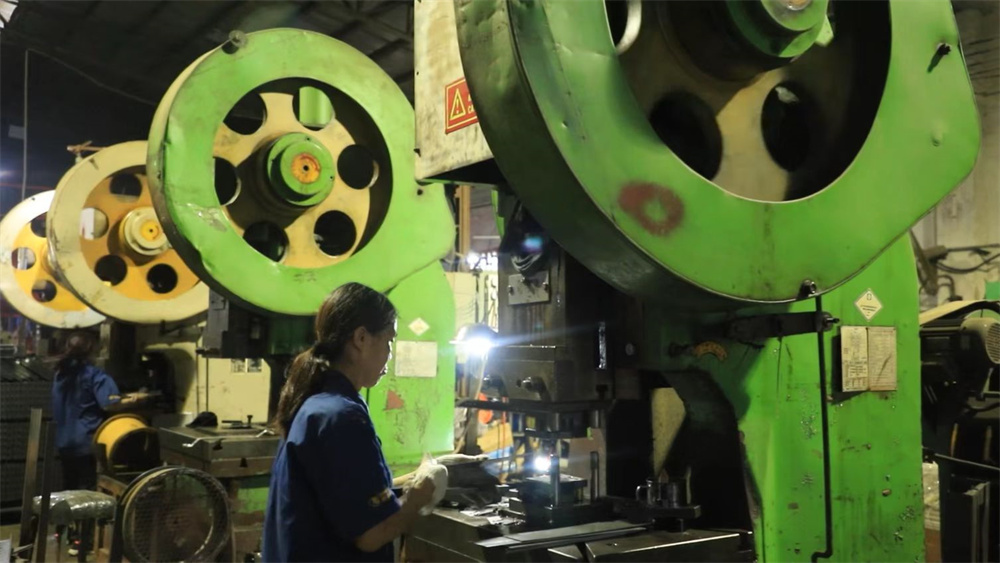
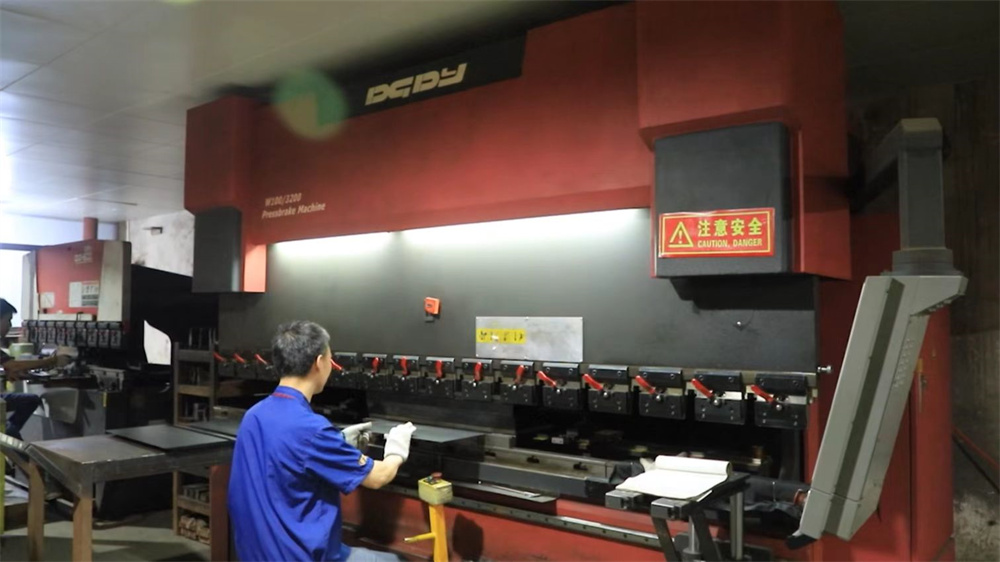
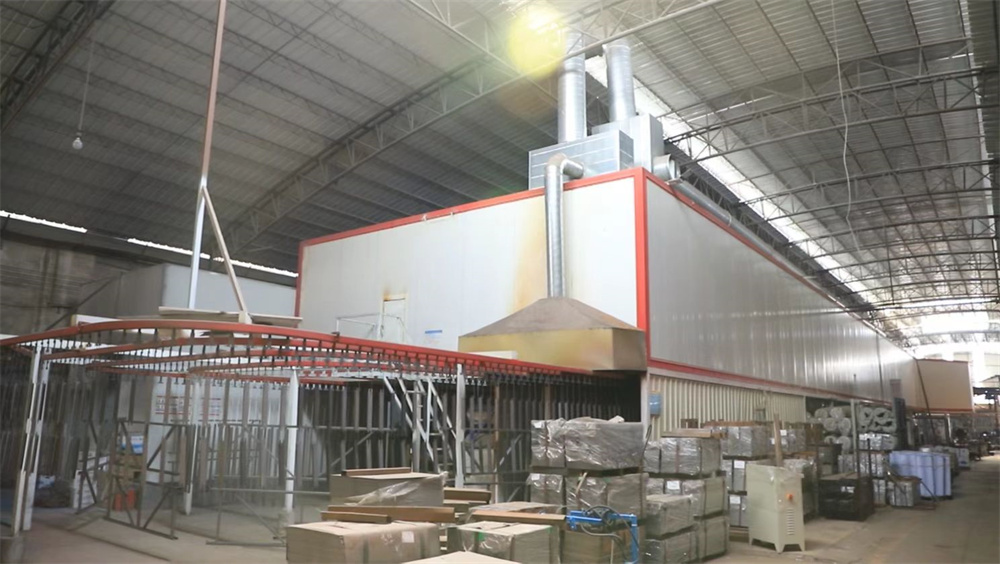
The primary advantage lies in the Agile Manufacturing Response (AMR). Unlike traditional Western manufacturers who may have lead times exceeding 16 weeks, Chinese facilities utilize integrated automation—from laser cutting to electrostatic powder coating—to reduce production cycles to 3-4 weeks without compromising the structural integrity required by international RMI standards. Furthermore, the proximity to the Port of Shenzhen offers a logistical lever, reducing transit costs and enabling real-time shipping tracking for large-scale enterprise rollouts.
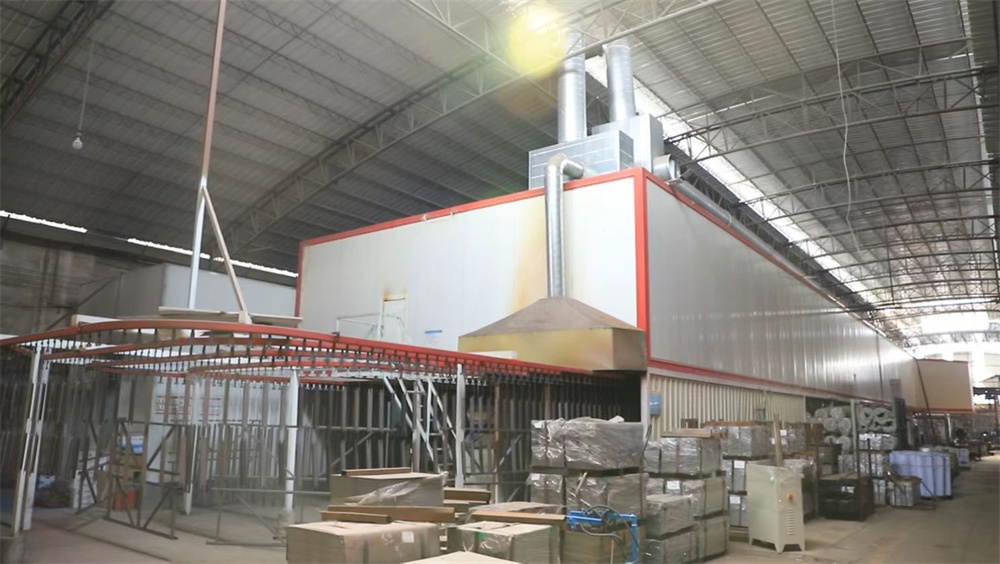
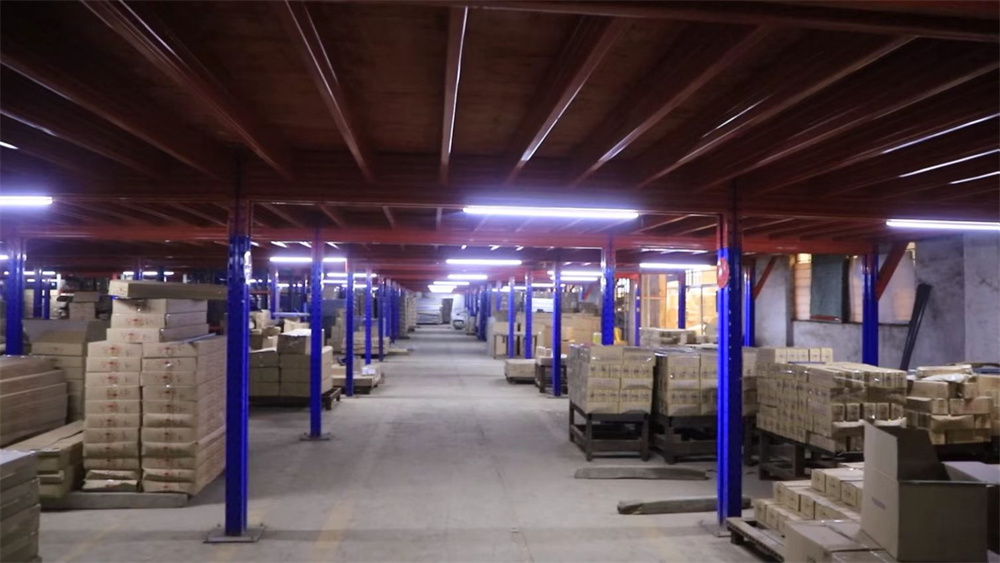
Established in 2015, Shenzhen Runda Racking Manufacturing Co., Ltd. is a premier manufacturer specializing in heavy-duty industrial shelving and high-density warehouse storage solutions. With over 11 years of deep industry expertise and 9 years of active global export experience, we deliver tailored racking systems to logistics hubs, distribution centers, and manufacturing plants worldwide. Operating from a modern 35,000 square meter production facility, our operations are powered by a robust network of over 1,200 trusted supply chain partners. This enables us to achieve an annual export turnover of $28 million. Our primary markets span North America, Western Europe, Southeast Asia, and the Middle East, where we proudly serve industrial distributors, large-scale third-party logistics (3PL) operators, and direct enterprise buyers.
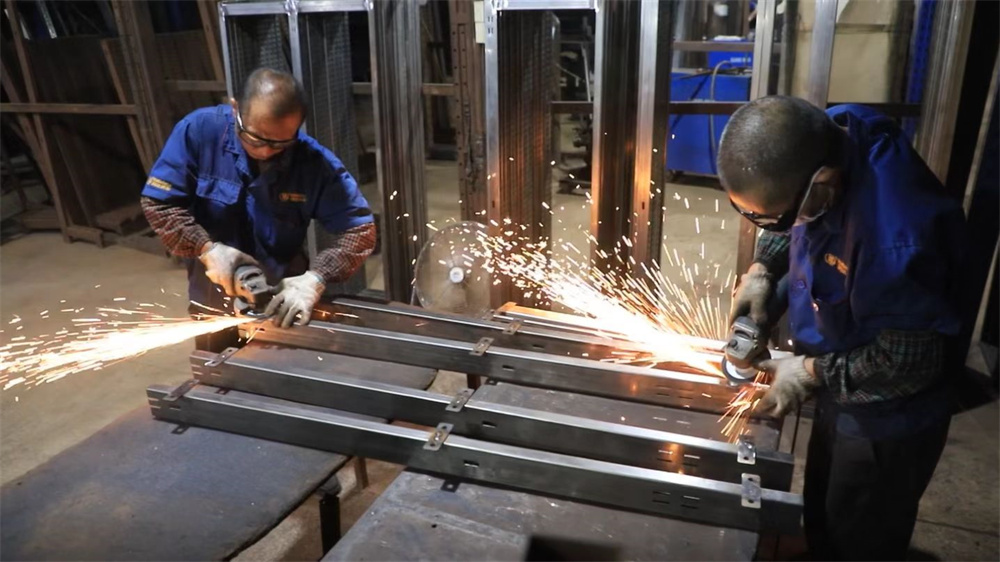
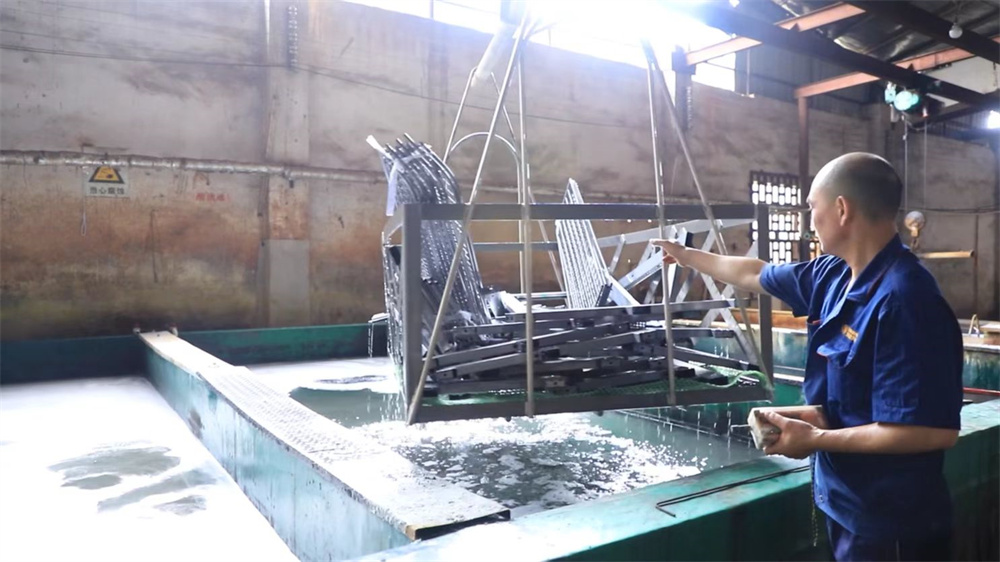
Quality and innovation drive our core philosophy. We maintain strict quality control through full-process sampling inspection, raw material stress testing, and load-bearing verification, backed by a dedicated team of 35 QC professionals. Innovation is led by our 18 experienced R&D engineers who continuously refine structural efficiency—releasing over 120 new and upgraded storage products last year alone. We offer comprehensive OEM/ODM and full custom manufacturing services, including tailored load capacities, custom dimensions, corrosion-resistant powder coatings, and specialized seismic structural designs.
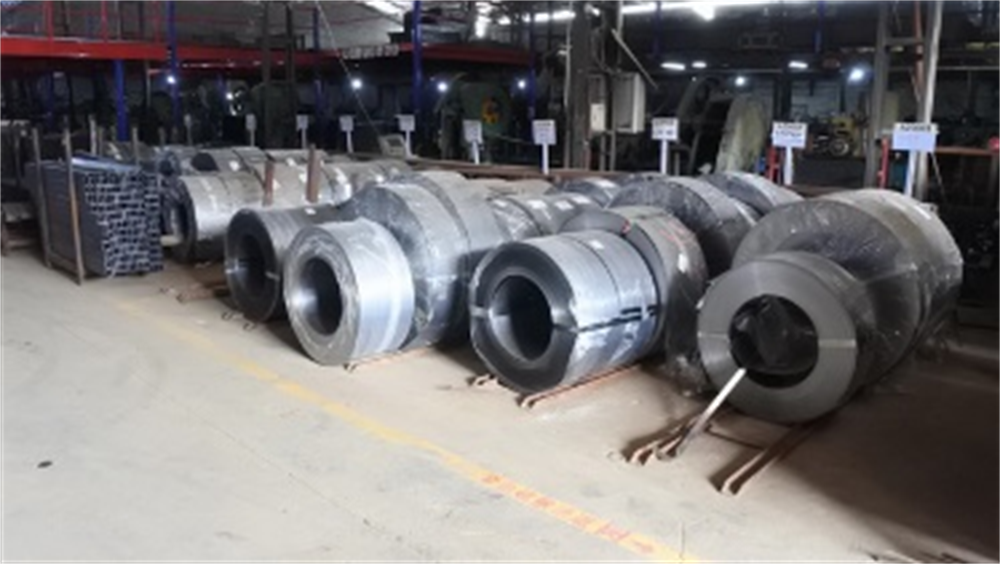
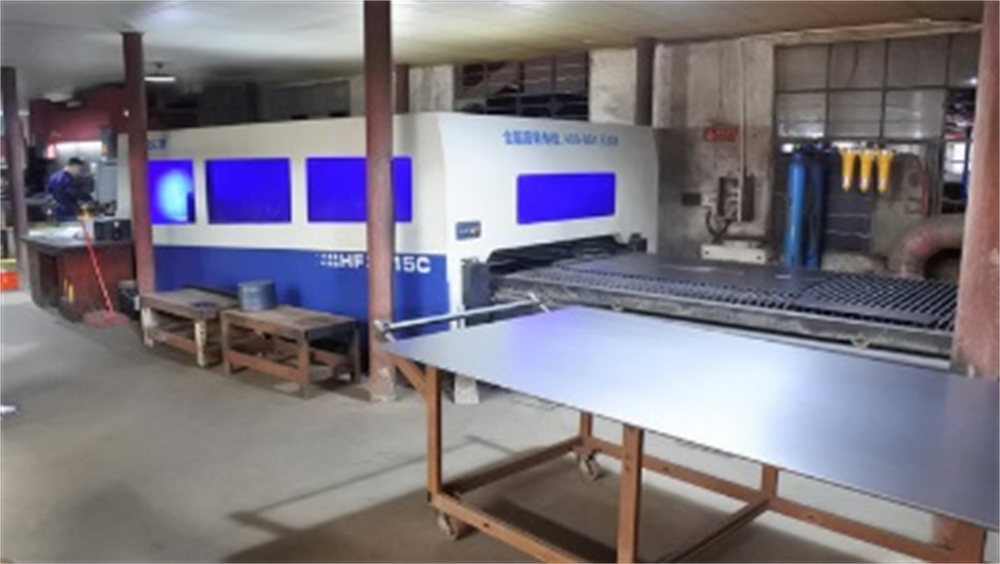
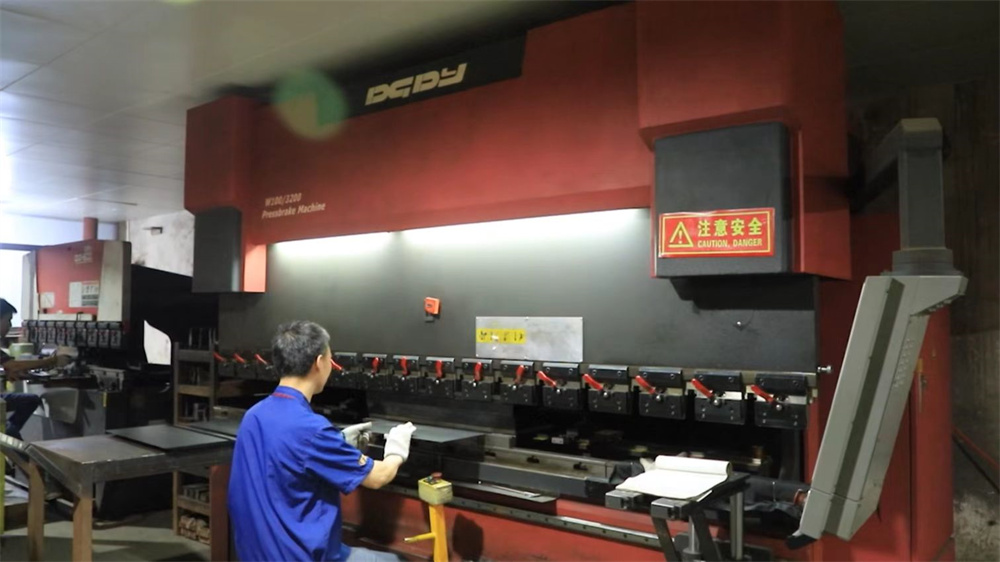
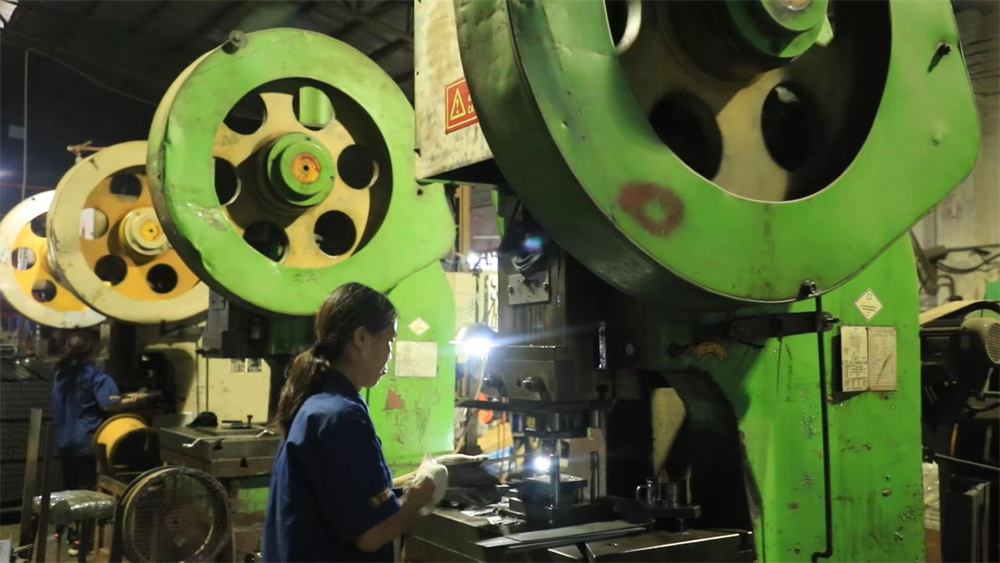
Integration of AS/RS (Automated Storage and Retrieval Systems) compatible shelving is no longer a luxury but a necessity for the "Dark Warehouse" era. We focus on millimetric precision to ensure robot-compatibility.
Specially treated galvanized finishes and alloy compositions designed for sub-zero environments, preventing structural embrittlement in refrigerated logistics hubs.
Utilizing high-tensile steel and specialized footplate designs to meet stringent seismic codes in regions like Southeast Asia and Western USA.
For procurement managers at Fortune 500 companies and 3PL providers, the primary pain point is not the cost per unit, but the Total Cost of Ownership (TCO). Our approach addresses this through:
 Runda Racking