High-performance commercial shelving engineered for maximum load durability, visual merchandising efficiency, and rapid retail deployment.
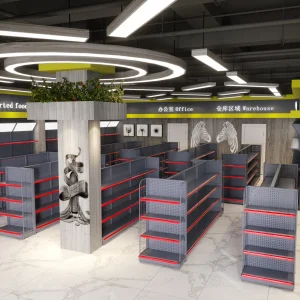
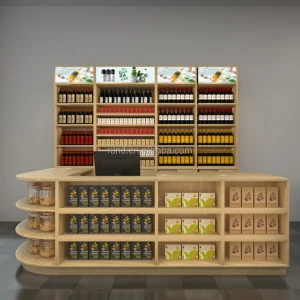
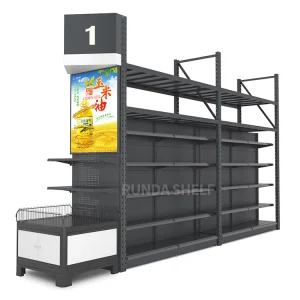
In today's globalized supply chain ecosystem, industrial steel storage racks and commercial gondola systems serve as the critical physical infrastructure supporting high-density warehousing, third-party logistics (3PL), dynamic fulfillment centers, and large-scale retail distribution. Evaluating a CE Certified Metal Racks Manufacturer & Supplier goes beyond assessing raw structural steel price per kilogram; it requires rigorous verification of structural load dynamics, safety factor margins, European Harmonized Standards compliance (such as EN 15512, EN 15635, and EN 1090-1), and environmental durability under dynamic working cycles.
Mandates limit state design principles for steel static storage systems. Our structural engineers compute elastic-plastic sway stability, beam deflection limits (L/200), and upright frame buckling safety margins under full vertical and horizontal seismic shear forces.
Factory Production Control (FPC) compliance certified for structural steel components. Ensures traceable raw material chemistry (Q235B / Q355B cold-rolled structural steel), standardized weld seam inspection, and rigorous non-destructive testing (NDT).
Engineering optimization reduces steel tare weight without compromising yield strength. Advanced thermosetting epoxy-polyester powder coating delivers superior anti-corrosion retention, lowering maintenance overhead over a 20-year structural lifespan.
A world-class industrial racking manufacturer delivering advanced warehouse storage infrastructure and customized commercial retail fixtures to global enterprises.
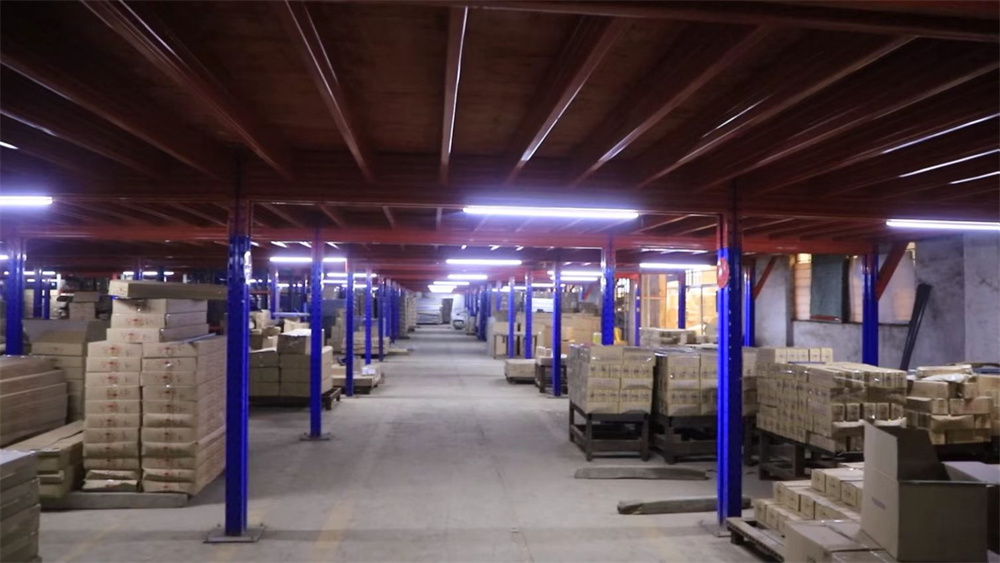
Established in 2015, Shenzhen Runda Racking Manufacturing Co., Ltd. has established itself as a premier global manufacturer specializing in heavy-duty industrial shelving, automated pallet racking, and high-density warehouse storage systems. With over 11 years of deep domain engineering expertise and 9 years of direct international export operations, we deliver tailormade racking structures to complex logistics hubs, cold-storage facilities, distribution centers, and commercial retail chains globally. Operating from our state-of-the-art 35,000 square meter manufacturing plant, supported by over 1,200 verified supply chain ecosystem partners, we achieve an annual export turnover exceeding $28 Million across North America, Western Europe, Southeast Asia, and the Middle East.
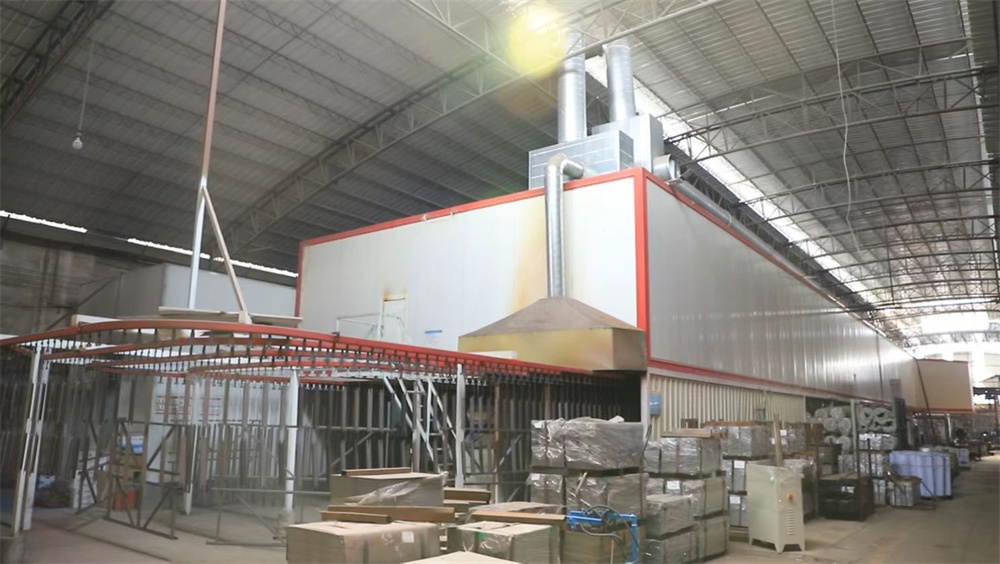
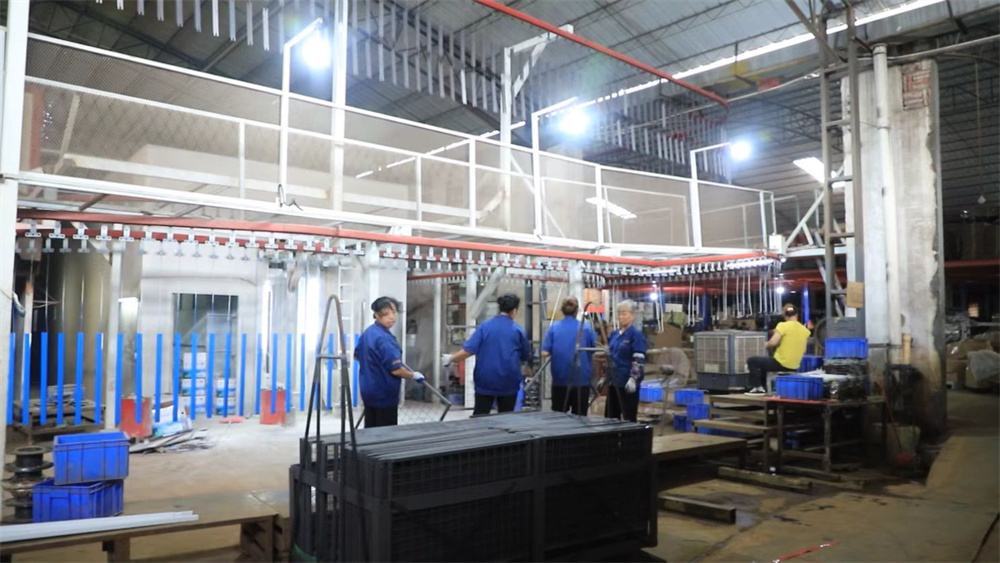
From certified raw material testing to automated electrostatic painting, our 13-stage manufacturing process guarantees unmatched structural tolerance and finish quality.
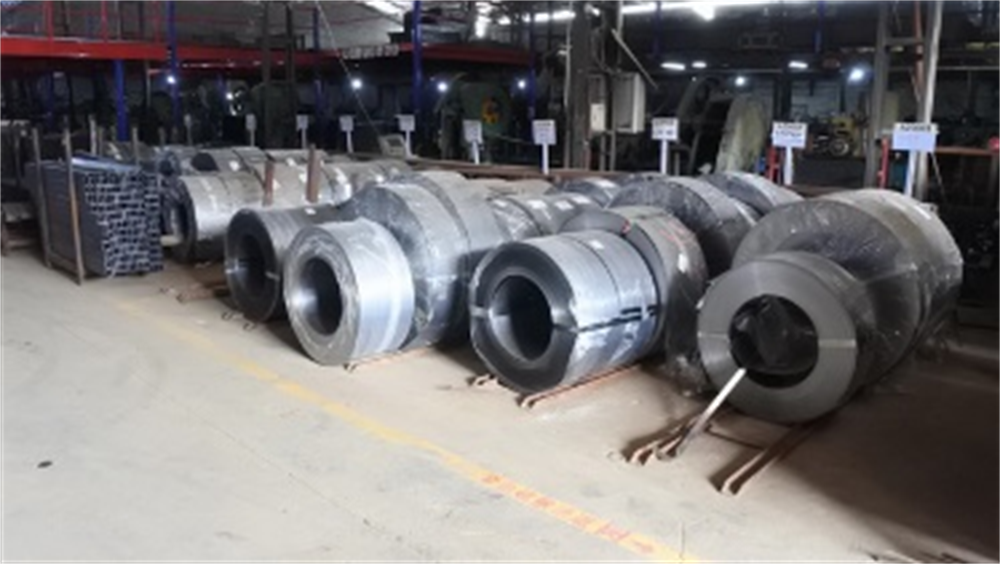
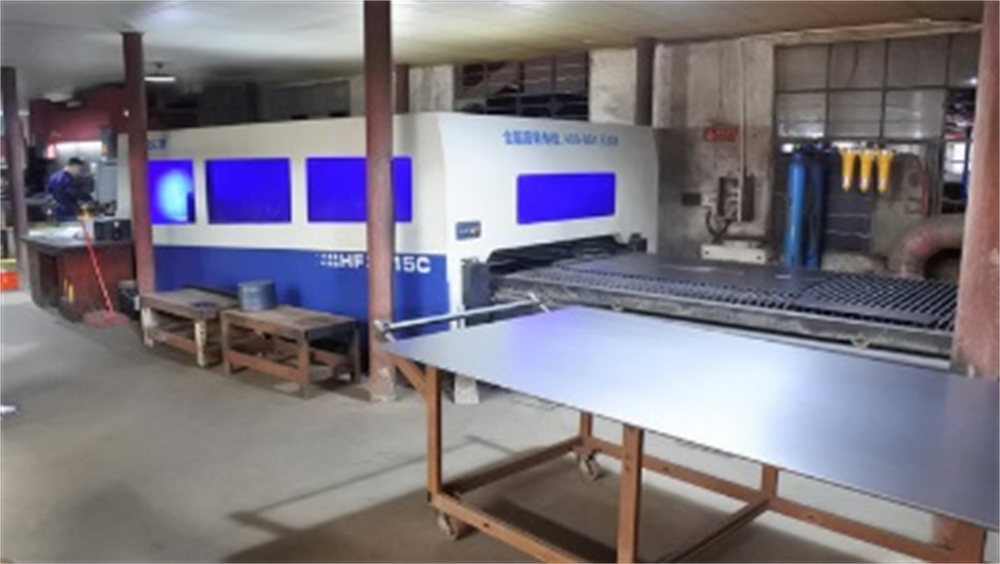
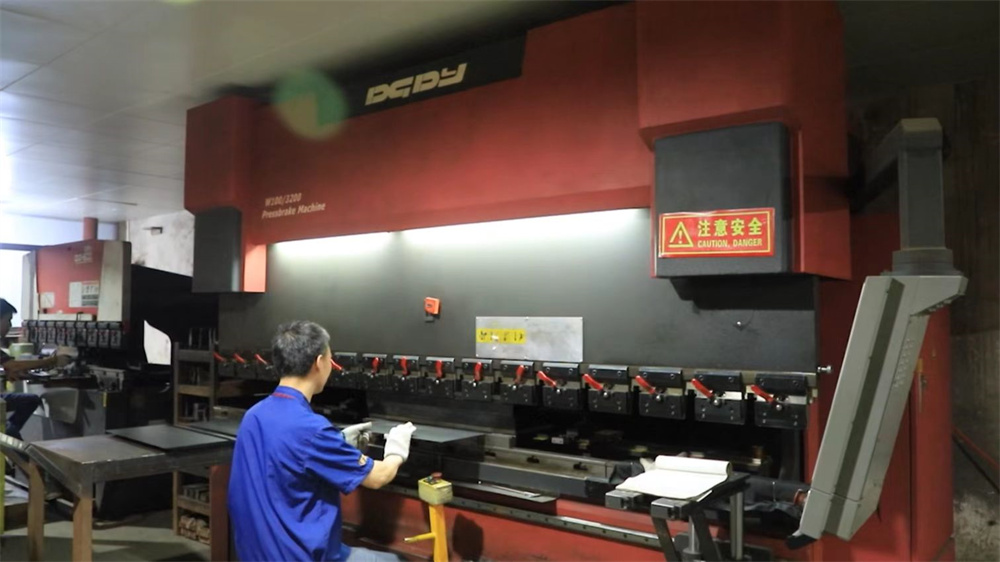
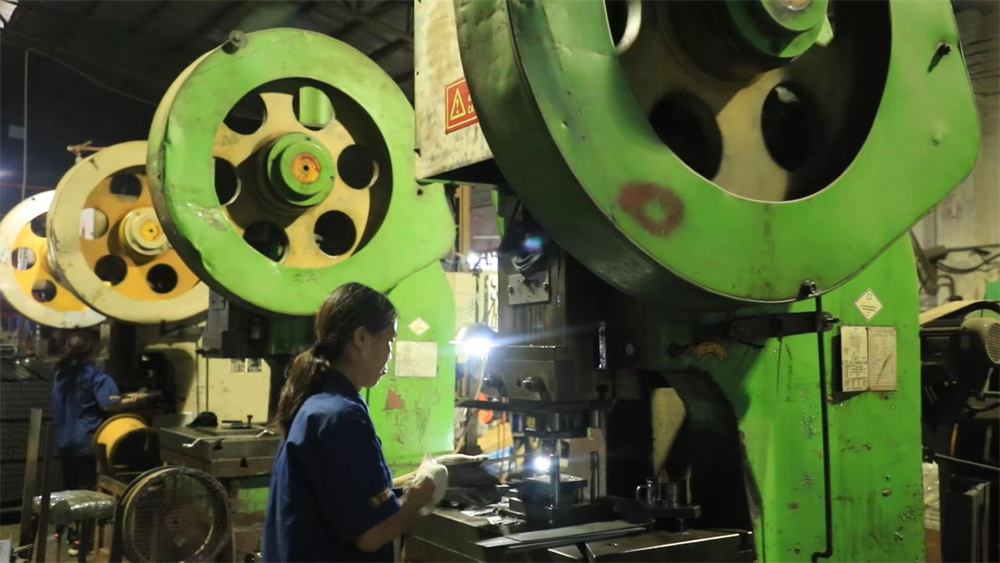
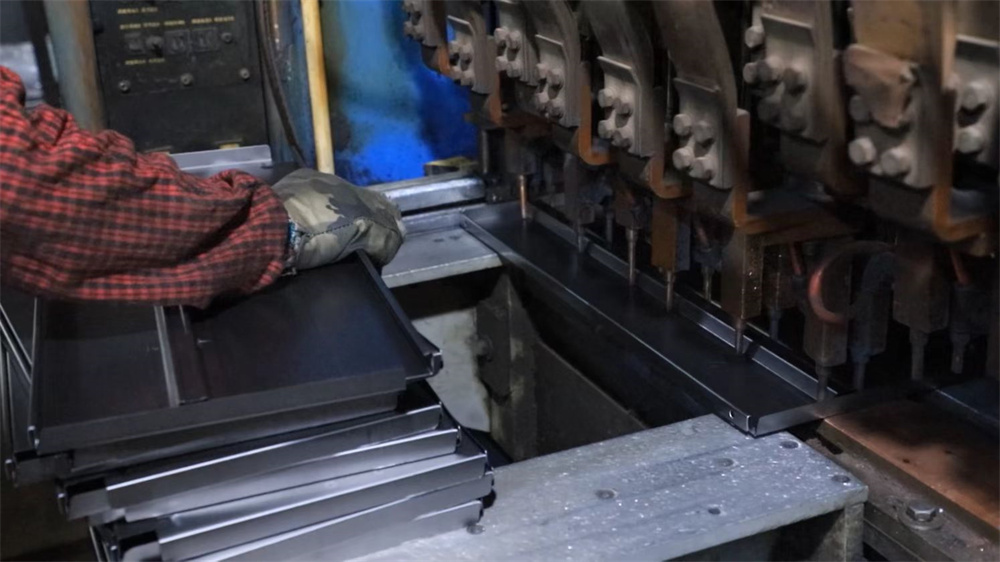
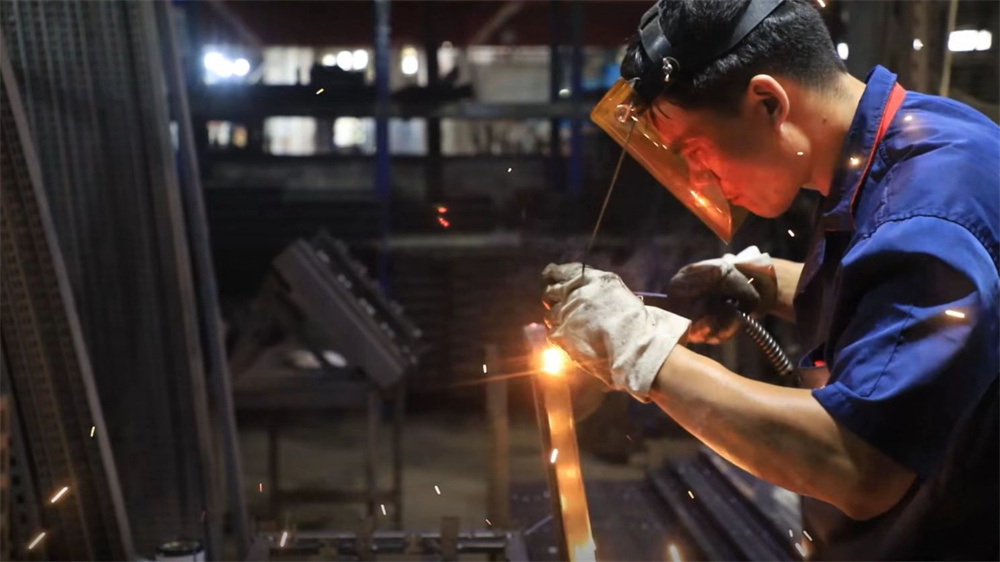
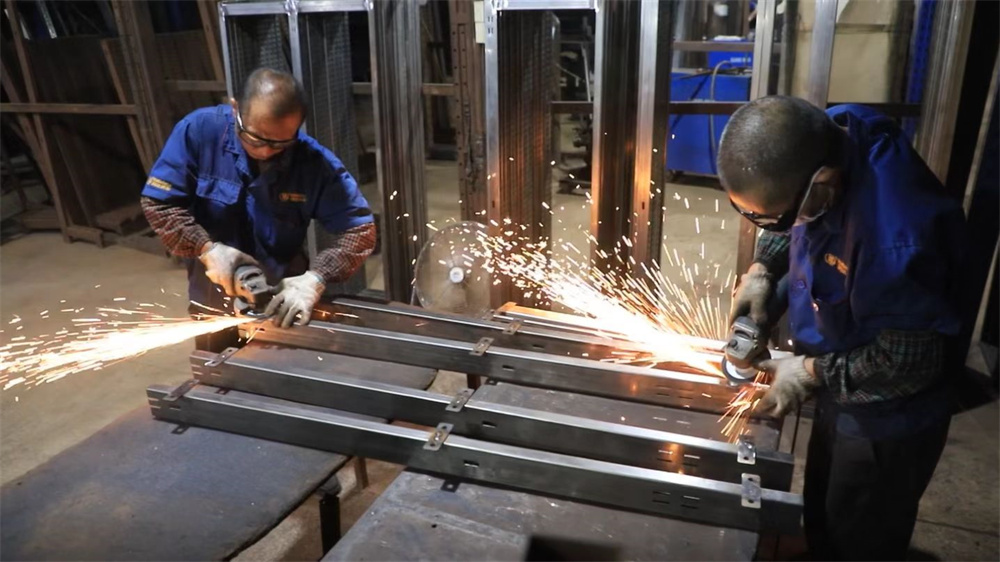
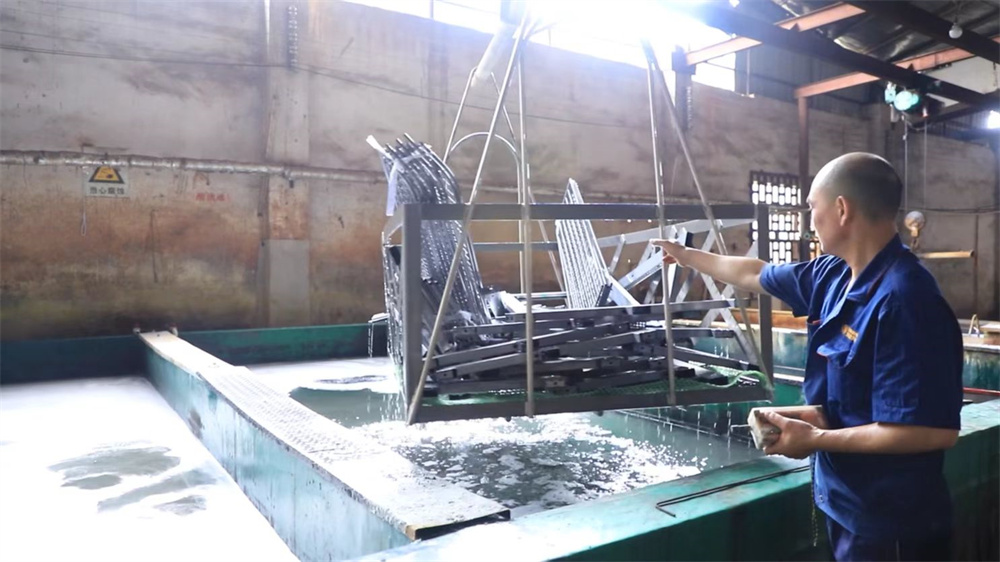
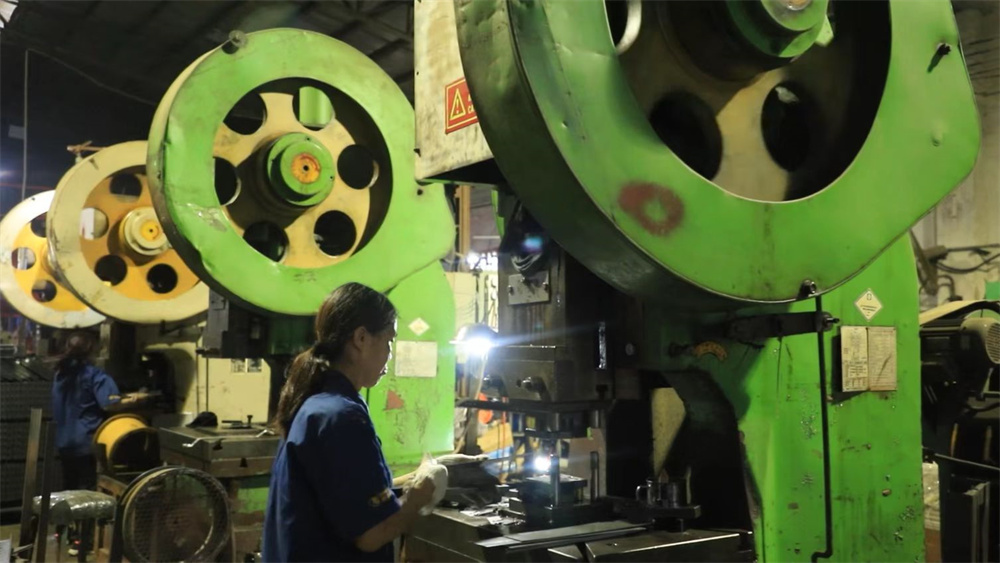
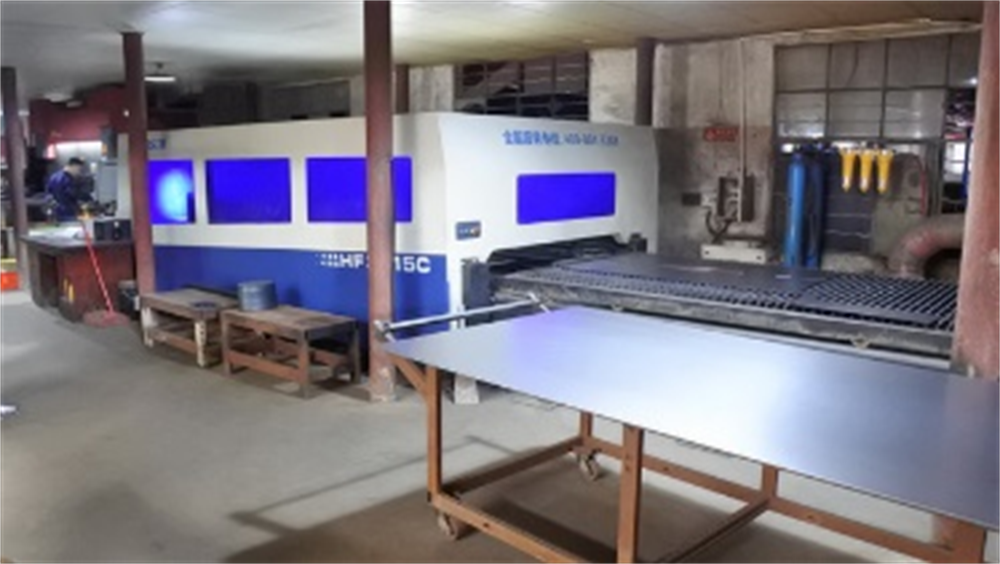
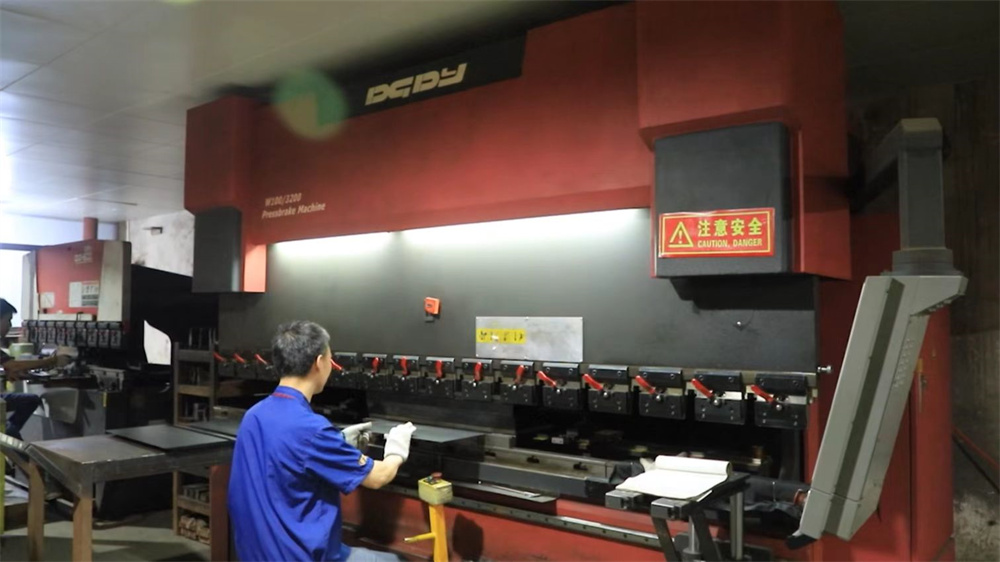
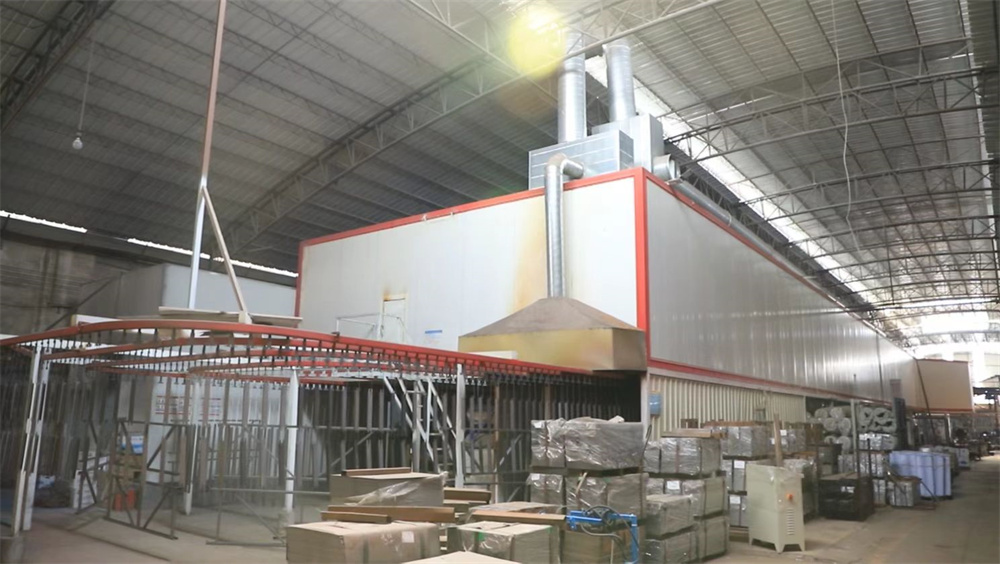
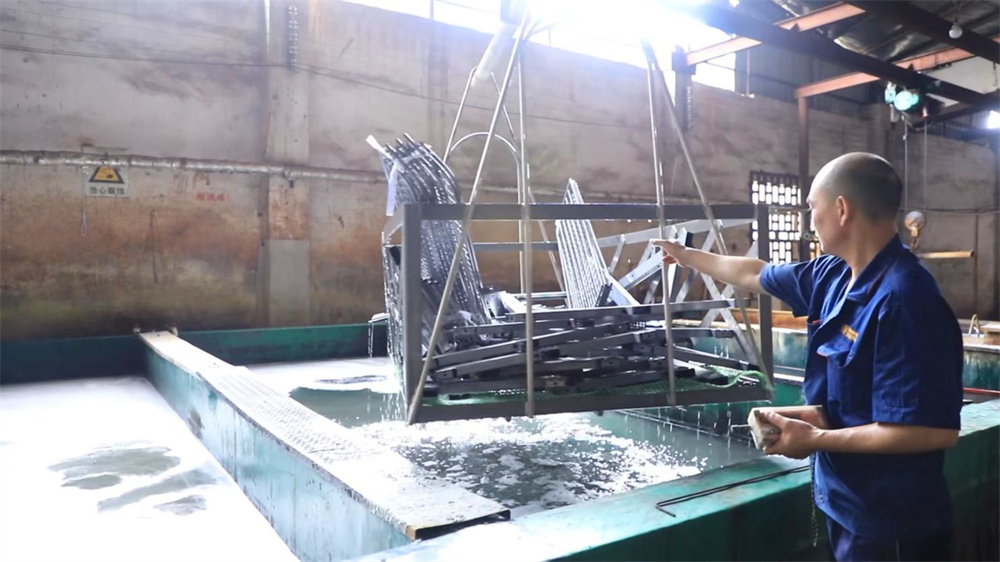
Ensuring structural integrity, seismic stability, and regulatory compliance for international industrial installations.
Our steel racking products carry full CE certification in compliance with the EU Construction Products Regulation (CPR). Mill Test Reports (MTR) according to EN 10204 3.1 are provided for every steel coil batch, ensuring total mechanical integrity and chemical composition verification.
Designed in accordance with European FEM 10.2.02 recommendations and US RMI (Rack Manufacturers Institute) standards. Structural calculations account for dynamic acceleration, baseplate floor anchor shear loads, and upright frame flexural rigidity.
Our 35-person specialized Quality Control division executes rigorous raw material tensile testing, weld seam ultrasonic flaw detection, coating cross-hatch adhesion tests, and full destructive load testing to 150% of rated capacity.
Leveraging Shenzhen’s technology ecosystem and Guangdong’s steel manufacturing clusters to offer unprecedented value and delivery speed.
Through strategic long-term contracts with premier steel mills (such as Baosteel and Shougang), Shenzhen Runda secures high-grade Q235B and Q355B structural steel at preferential volume tariffs. Over 1,200 integrated supply chain partners allow rapid scale-up for mega-warehouse contracts without supply bottlenecks.
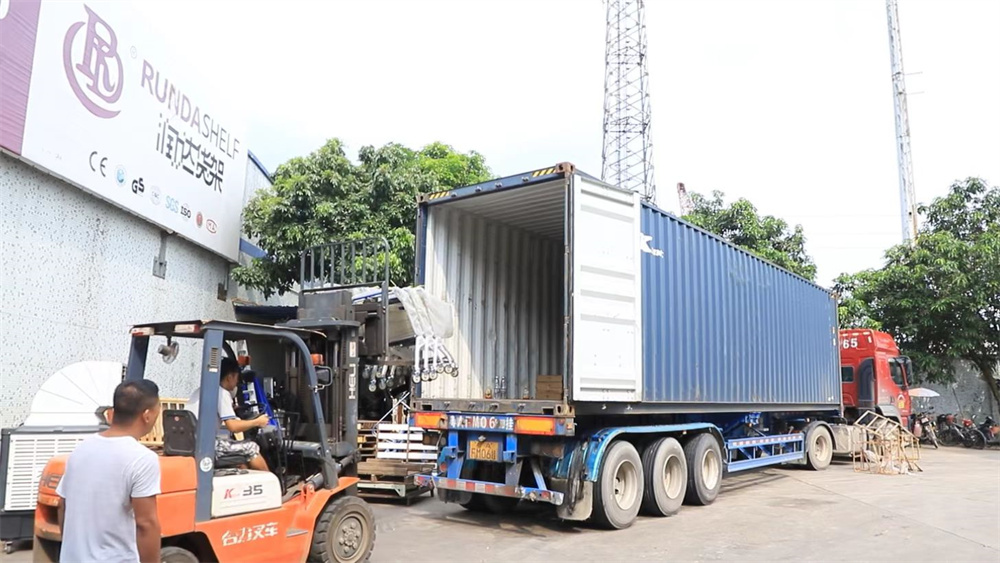
Located in Shenzhen, adjacent to Yantian and Shekou deep-water ports, we eliminate domestic transport friction. Our dedicated international logistics trade team handles export clearance, sea freight container consolidation, and door-to-door DDP shipments for global procurement buyers.
Adapting metal racking engineering to automated systems, environmental sustainability, and omni-channel logistics speed.
Transitioning from traditional manual pallet racking to Automated Storage and Retrieval Systems (AS/RS). We engineer ultra-precise beam profiles with deflection tolerances within ±1.5mm to interface seamlessly with robotic stacker cranes and AGVs.
Zero-VOC, heavy-metal-free electrostatic powder coating lines. Our closed-loop curing ovens reduce energy consumption per ton by 22%, meeting stringent international environmental protection regulations and ESG corporate requirements.
Dynamic supply chains require adaptable layouts. Our teardrop and 50mm/75mm pitch beam connections allow rapid adjustment of beam levels without specialized tools, lowering reconfiguration time by up to 60%.
Engineered performance designed to meet specific operational requirements across key sectors.
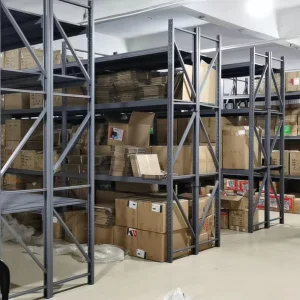
Selective and Drive-in Pallet Racks optimized for fast inventory turnover, high SKU density, and heavy-duty forklift operation (up to 4,000kg load per level).
Specialized low-temperature resistant steel formulations and galvanizing finishes that resist micro-cracking and rust formation in sub-zero refrigerated environments.
Heavy-duty longspan shelving, tire racking, and custom wire mesh decking tailored for asymmetric automotive spare parts and heavy engine components.
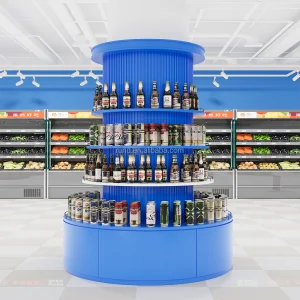
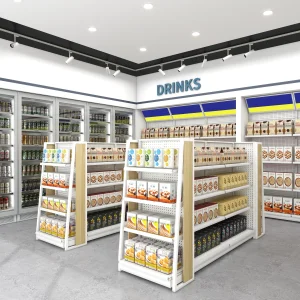
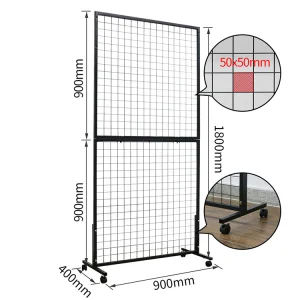
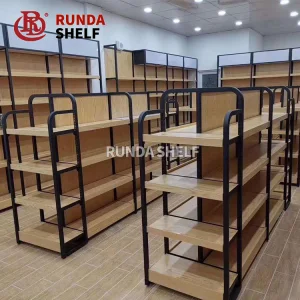
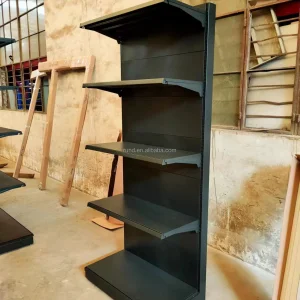
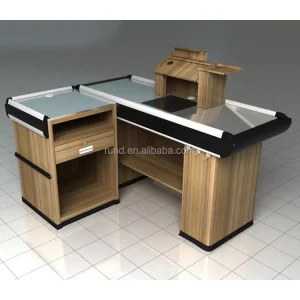
Modular steel-and-wood combination display gondolas, pegboard hook panels, and checkout counters combining high structural aesthetic with heavy foot-traffic resistance.
In-depth answers regarding CE certification, custom manufacturing, load limits, and international shipping.
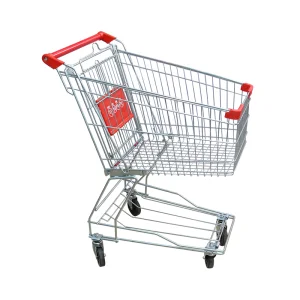
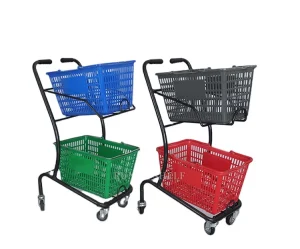
High-capacity warehouse racking, specialized tire racks, hydraulic material handling tools, and premium checkout systems.
 Runda Racking